Cooking tunnel for snacks and conveyor-belt products

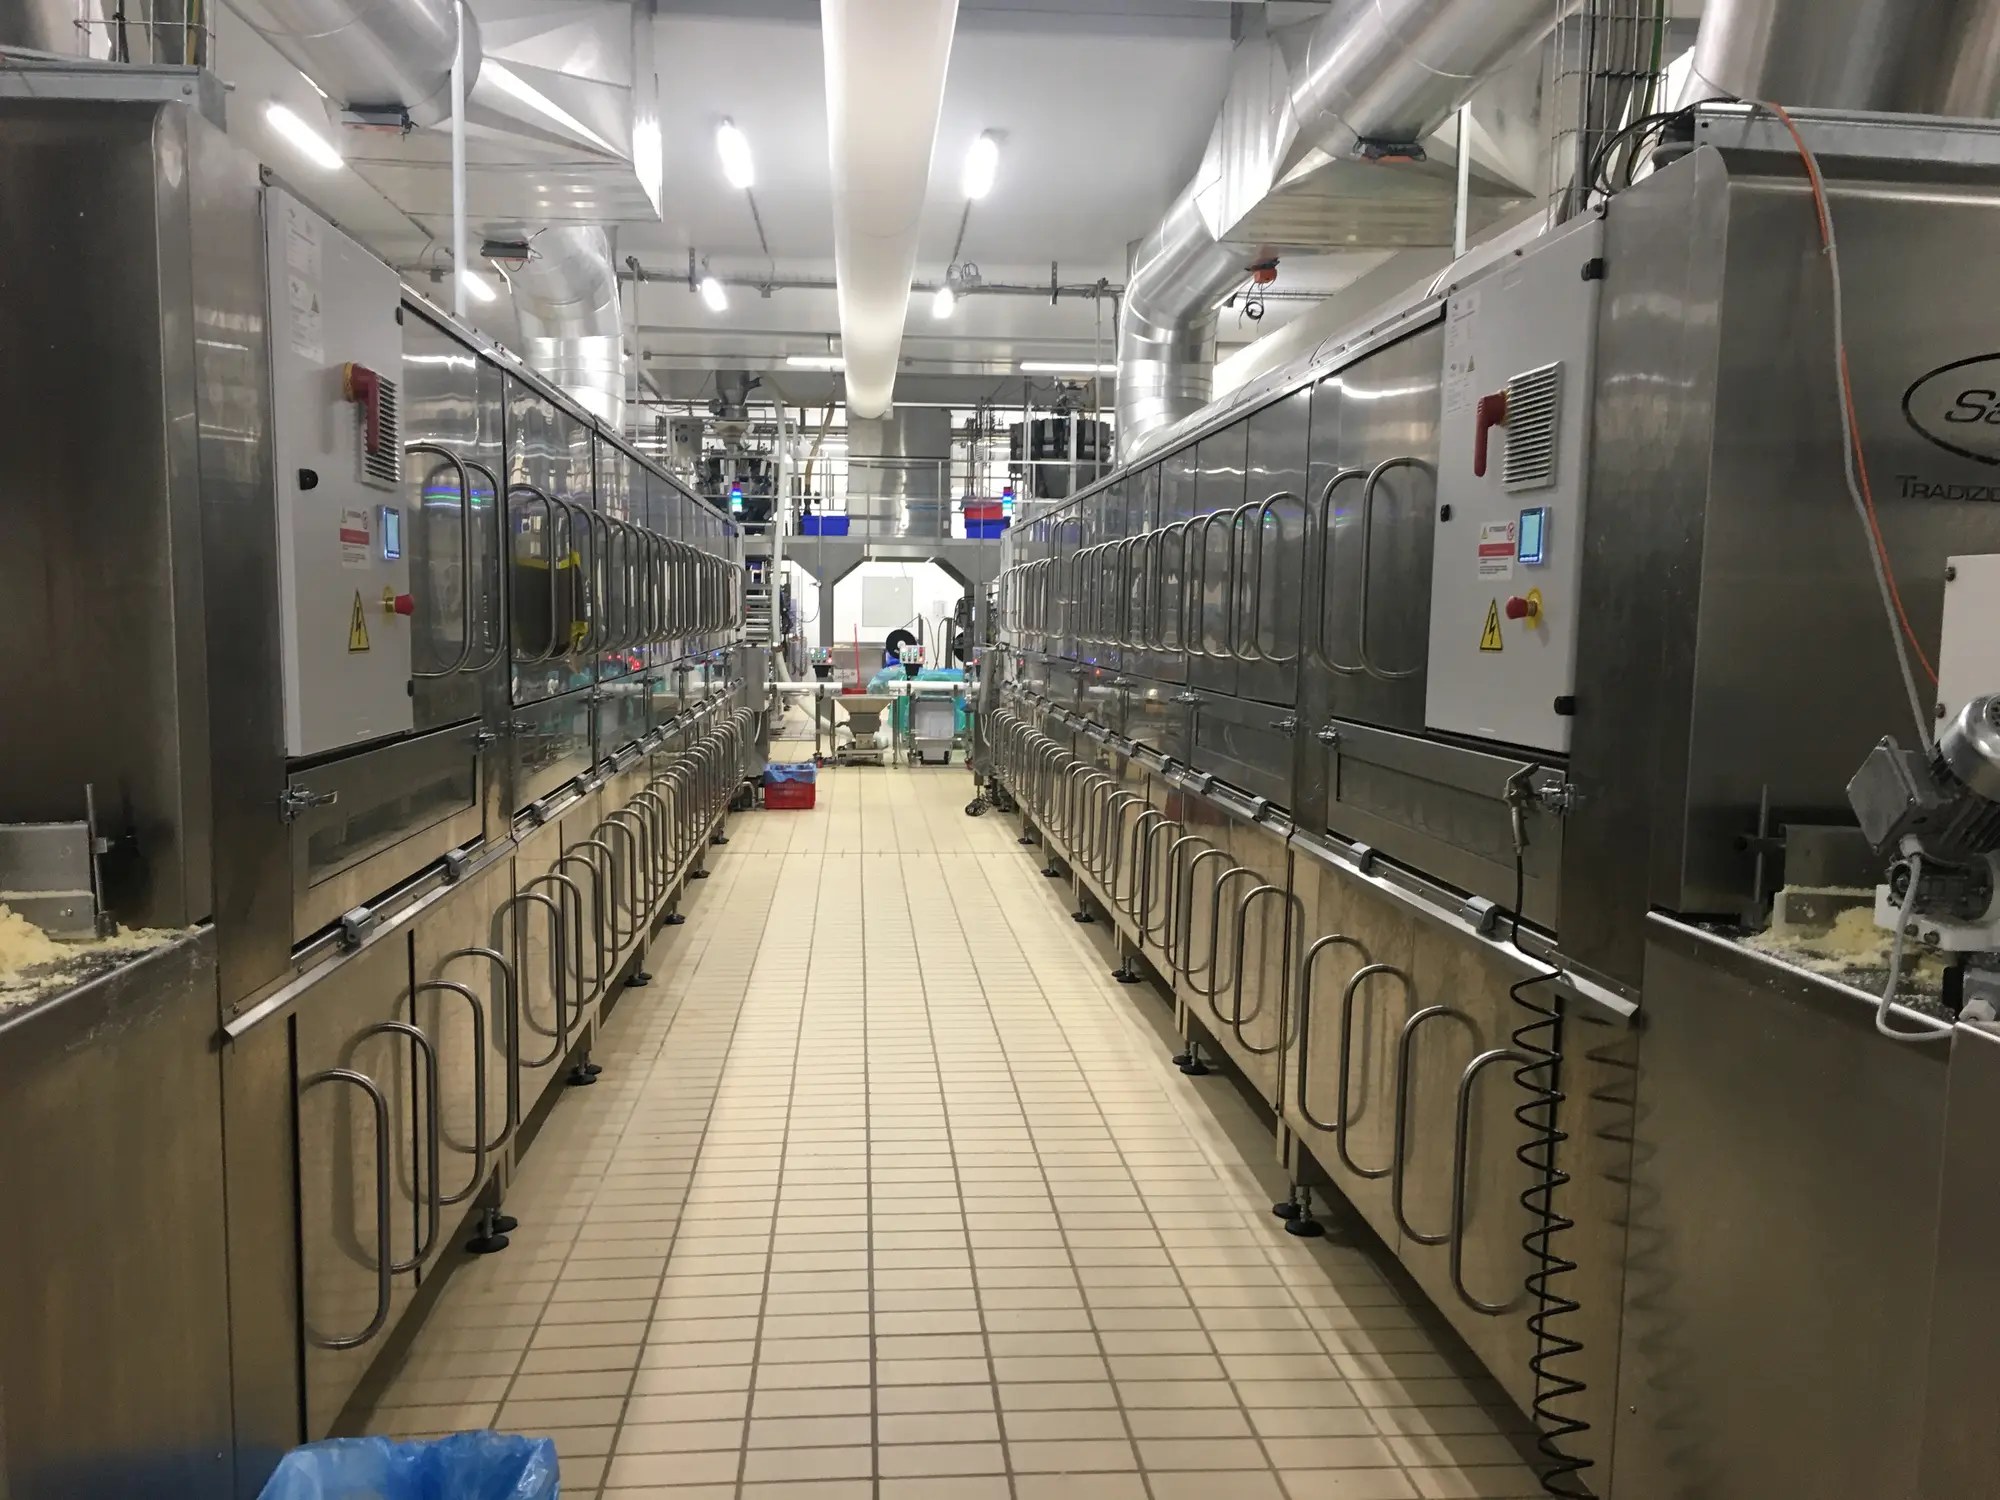
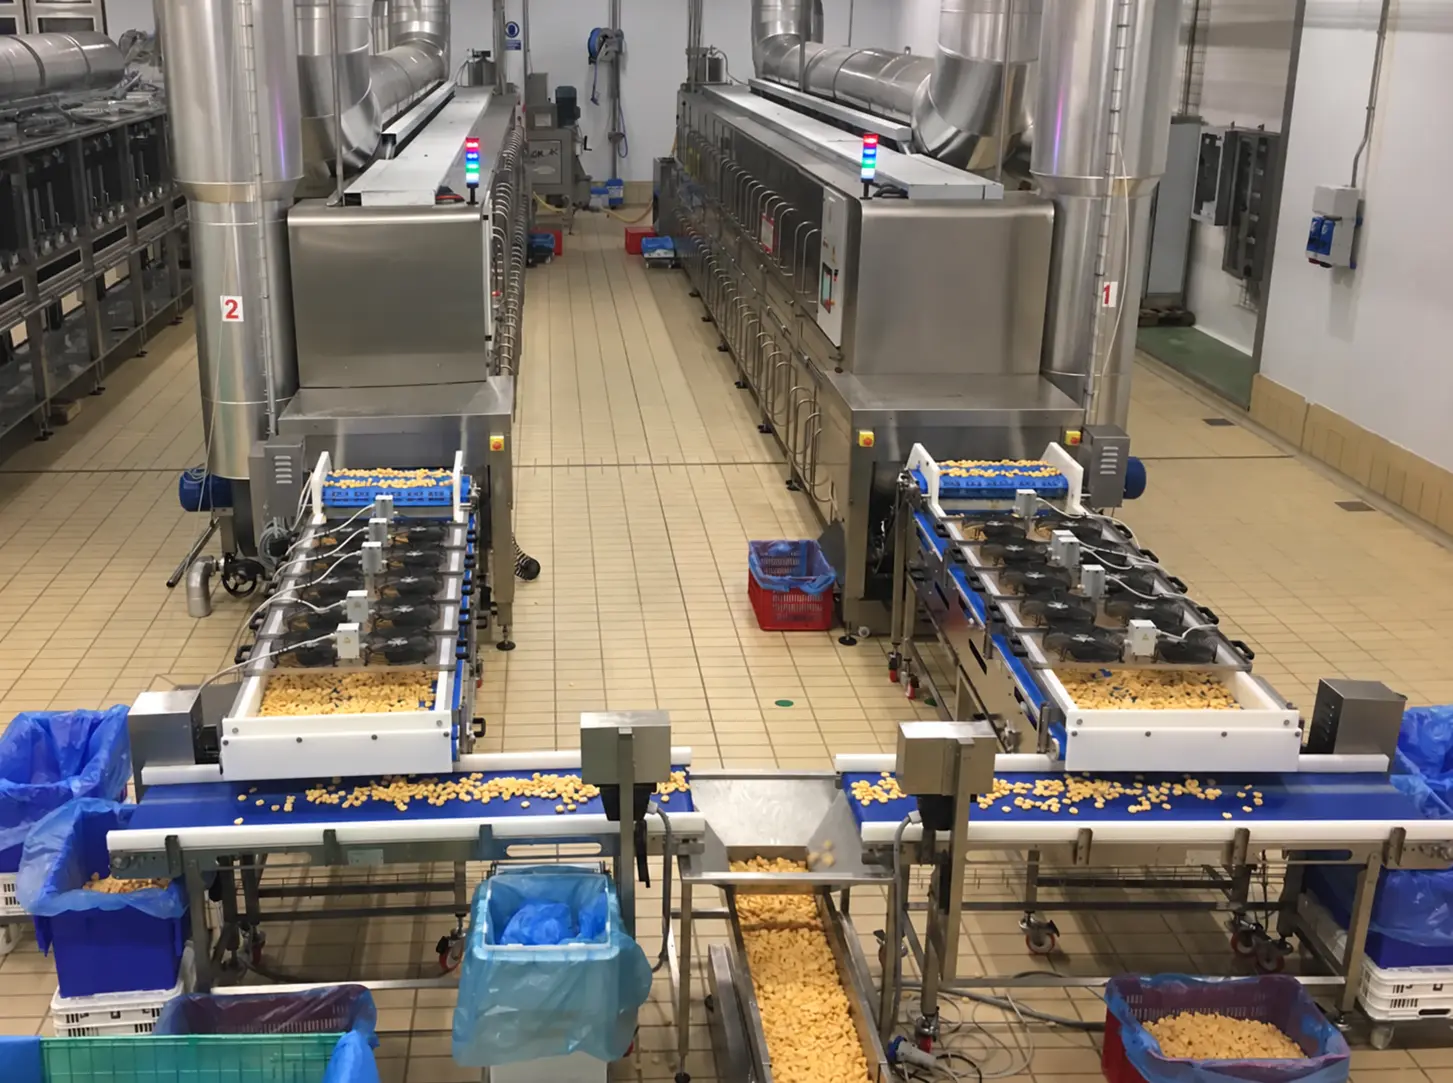
The cooking tunnel for snacks and food products is a continuous industrial oven designed to cook food products on a smooth or moulded conveyor belt through the combined action of microwave energy and hot air.

The two technologies work together inside the treatment chamber: microwave energy acts directly on the product, while the hot air flow completes the thermal process as the product moves through the oven.

The machine is designed for automatic operation within a production line, with products loaded and unloaded via a conveyor belt, and is equipped with a cooling module.

The tunnel is equipped with a continuous conveyor belt washing system.

Process
Cooking
Target throughput
> 40 kg/h
Technologies
Microwave + hot air

Applications

  • Cooking of food products in open packaging
  • Cooking of food products on a conveyor belt
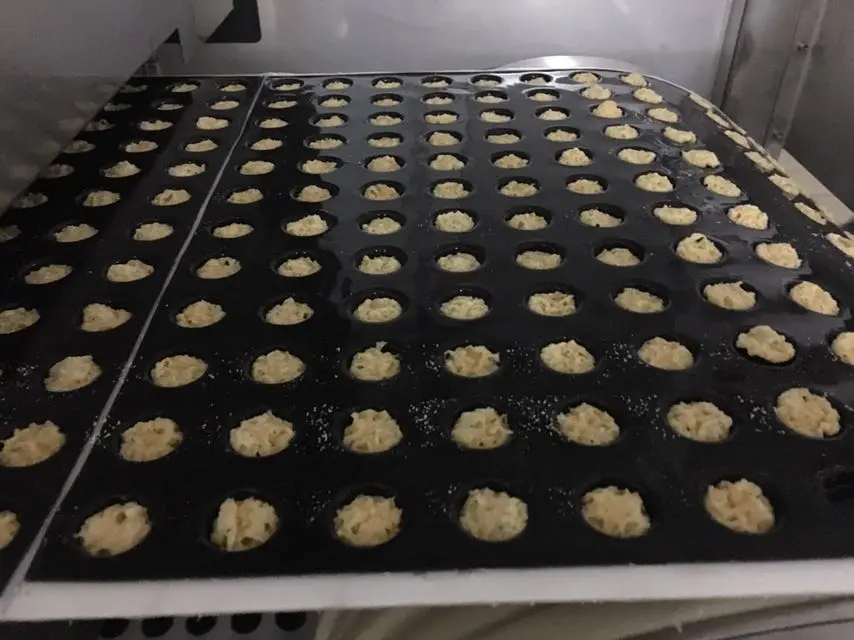
  • Snack cooking

How it works

The microwave and hot air tunnel is designed for continuous operation and to achieve an average throughput starting from 40 kg/h, depending on the product, packaging format and set process parameters.

Combined technology: focus on efficiency and maintainability

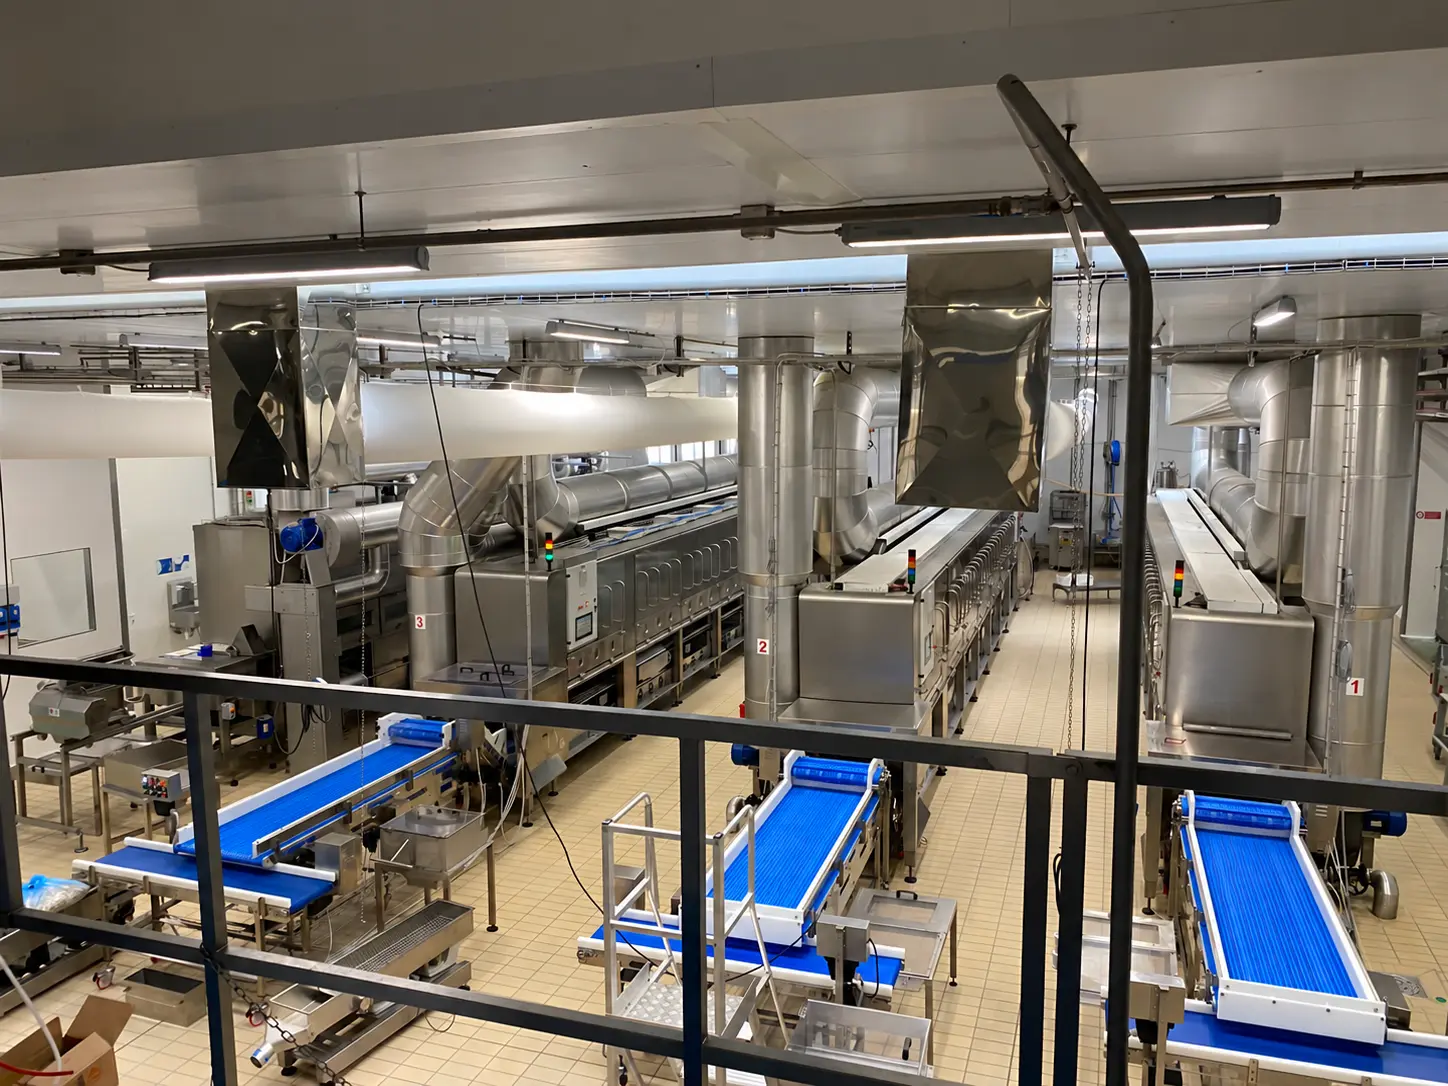
The snack cooking tunnel is a modular industrial machine designed for automated snack cooking and production.

The cooking process combines microwaves and hot air, while the product continuously passes through the different treatment chambers.

The modular configuration allows the oven to be integrated into an automated production line.

Microwaves

The machine consists of five microwave treatment chambers, in which microwave energy is used to cook the product as it moves through the oven.

Each cooking module is equipped with four microwave power supplies, providing a total nominal power of 80 kW. The power of each microwave emitter can be continuously adjusted via the operator panel, allowing the treatment to be configured according to the requirements of the production process.

Hot air, ventilation and recirculation

Microwave energy is combined with a hot air ventilation system, which contributes to cooking the product inside the chambers and ensures effective moisture removal.

The extracted air is filtered and, when necessary, further heated by electric heating elements before being introduced into the cooking chambers.

Air recovery

A distinctive feature of the oven is its ventilation system with energy recovery.

The system manages the various airflows required for the process, including magnetron cooling, hot air supply to the chambers, conveyor belt drying and fume extraction.

Part of the thermal energy contained in the airflows is recovered and reused within the ventilation system.

Modularity

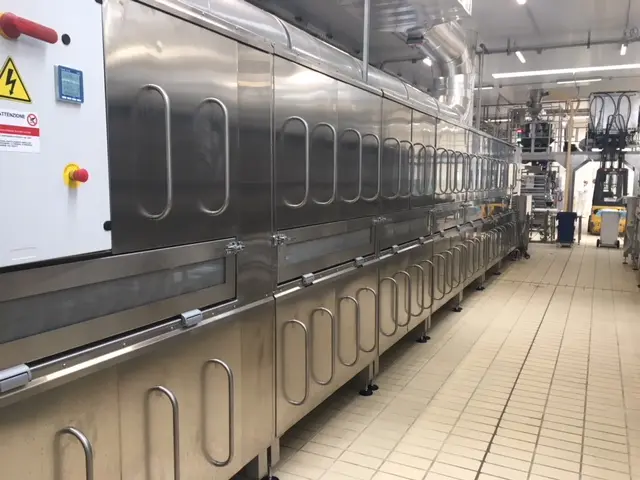
The oven consists of a series of food-grade stainless steel modules connected together to form the treatment tunnel.

The machine includes an infeed section, an outfeed section, attenuator modules and five cooking modules, where the combined microwave and hot air treatment takes place.

The modular structure allows the different process stages and the systems required for machine operation to be arranged efficiently.

Conveyor belt customisation and cleaning

The product passes through the cooking chambers on a continuous silicone conveyor belt, 600 mm wide, suitable for food contact, process temperatures and use in a microwave environment.

The conveyor drive system is equipped with automatic tensioning to compensate for dimensional changes in the belt caused by temperature variations. The oven also incorporates a dedicated conveyor belt cleaning and drying system, located in the lower section of the modules, which operates continuously while the tunnel is running.

Safety and reliability

The cooking chambers are equipped with doors, on both sides, that can be fully opened to 180°. This configuration allows visual monitoring of the cooking process and provides easy access to the treatment area, facilitating oven cleaning, sanitisation and maintenance.

The attenuator modules feature specially designed, patented microwave field attenuation systems that require neither hydraulic circuits nor maintenance.

Integration and control

The oven is operated via an operator panel, which allows the main machine systems to be controlled easily and intuitively, and the operation of the microwave sources to be adjusted. In particular, the system allows the power level of each magnetron to be continuously adjusted and the main operating parameters to be monitored.

The tunnel can be connected to factory management systems.

Technical specifications

Main technical specifications of the reference configuration.

Type
Modular snack cooking tunnel
Application
Food products for snack production
Structure
Stainless steel
Inspection doors
Doors opening up to 180°, equipped with inspection windows
Treatment technology
Microwave and hot air
Control system
Touch screen control panel
Installed microwave power
96 kW
Installed fan power
24 kW
Installed heating element power
24 kW
Individual microwave generator power
1 kW
Installed electrical power
≈ 170 kVA
Compressed air supply pressure
≈ 6 bar
Conveyor belt speed
0.8÷3.5 m/min
Adjustable air temperature
20÷90 °C
Conveyor belt width
600 mm
Maximum overall length
14,370 mm
Maximum overall width
2,045 mm
Maximum operating height
2,980 mm
Loading height
1,030 mm

Industrial microwave systems designed for measurable performance, flexible packaging and 24/7 production

1

Measurable performance

Desk studies, sizing assessments and energy calculations are carried out before project development. Expected performance is verified through in-house testing on actual products.

2

Packaging flexibility

Compatible with microwave-safe, non-metallic packaging, without restrictions to proprietary trays, films or valves. Packaging is selected according to the product.

3

Industrial automation

Recipes, traceability, temperature control, data logging, alarms, remote assistance and integration with existing production lines.

4

Proprietary technology

Microwave applicators, shielding systems, and command and control systems developed in-house to ensure safety, stability, durability and ease of maintenance.

5

24/7 operation and independent maintenance

Accessible components, clear diagnostics, identifiable spare parts and operator training: the system is designed to allow customers to carry out routine maintenance in-house, reducing downtime and dependence on the supplier.

6

Validated quality

Texture, colour, nutrients, clean-label characteristics and shelf life are verified through testing and validation.

MIPAAF Validation

Microwave technology for organic

Validated cooking and pasteurisation processes for organic production.

CookingPasteurisationOrganic

Download

Download the catalogue dedicated to cooking and pasteurisation and the appendix featuring practical applications.

Cooking and pasteurisation catalogue 2026 cover

Cooking and pasteurisation

2026 catalogue featuring solutions, technologies and configurations for industrial processes.

Download the catalogue
Cooking and pasteurisation applications appendix cover

Cooking and pasteurisation case studies

Appendix featuring industrial applications and combined microwave processes.

Download the appendix